Technology
PEM pure-water electrolysis, two separate gas channels, multi-stage flame suppression and terminal mixing.
State-of-the-art PEM pure-water electrolysis
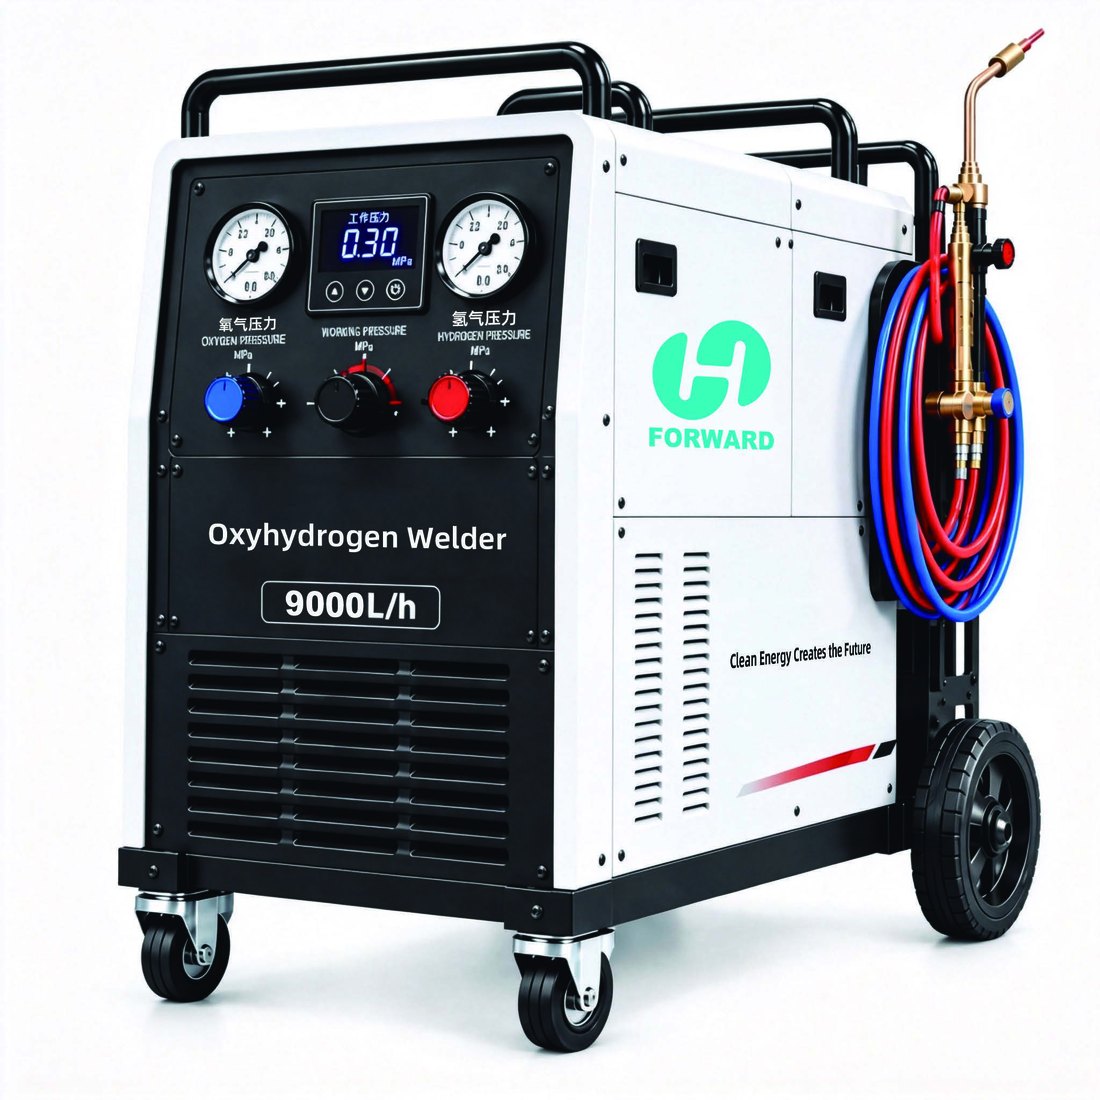
Hydrogen and oxygen are generated in separate channels inside a proton-exchange-membrane stack, with two independent gas–liquid separators. The gases travel through their own pipelines and are mixed for combustion at the torch tip — never inside the machine.
Because the machine stores no pressurised gas and mixes nothing internally, it removes the two classic failure modes of gas welding: high-pressure storage and an explosive mixture sitting in a tank.
Combustion outputs solely water vapour. There is no carbon, no alkaline mist and no toxic exhaust, which is why the flame can be used indoors, beside a production line or in a laboratory.
- Separate H₂ and O₂ channels inside the PEM stack
- Two independent gas–liquid separators
- Gases mix only at the torch nozzle
- No pressurised gas stored inside the machine
From pure water to a welding flame
Three stages, all inside one cabinet: generation, separation, combustion at the tip.
H₂ and O₂ travel through two independent pipelines and are mixed only at the torch nozzle, so no explosive mixture is ever stored inside the machine.
Oxyhydrogen versus acetylene and alkaline systems
The same comparison our customers run before they buy.
| Products | Traditional acetylene gas cylinder welding | Traditional alkaline electrolytic oxyhydrogen welding machine | FORWARD PEM pure-water machine |
|---|---|---|---|
| Fuel source | Gas in cylinders, purchased continuously. | Water + strong alkaline electrolyte. | Pure water + electricity — clean and easily available. |
| Gas generation principle | High risk of high-pressure gas storage. | Direct gas mixing inside the tank. | Separate gas production, terminal mixing only. |
| Safety characteristics | Likely to leak, flash back and explode. | Gas leakage hazard, pipeline corrosion. | Safe structure, multiple protection measures, no corrosion. |
| Flame | Black smoke and toxic exhaust gas. | No carbon, but alkaline mist pollution. | Only water vapour — zero pollution. |
| Welding effect | Carbonisation and discolouration, many defects. | Prone to alkali stains, needs cleaning afterwards. | Clean, bright weld points, no secondary pollution. |
| Cost | Extremely high. | Moderate maintenance cost, but expensive in the later stage. | Extremely low — the best long-term cost performance. |
| Site & qualifications | Requires a cylinder storage room and annual inspection of pressure vessels. | No cylinders needed, but alkaline storage and waste-liquid treatment are required. | Portable, flexible placement, no cylinder qualification and no hazardous waste treatment. |
In short: separate oxygen and hydrogen production lines, mixed only at the nozzle, reduce the risk of internal gas leakage. Pure-water electrolysis removes strong-alkali corrosion and alkaline mist pollution altogether.
Three steps from delivery to first weld
There is no installation crew, no gas contract and no pressure-vessel inspection to plan for.
Fill with pure water
Pure water goes into the tank. There is no electrolyte and nothing to mix.
Switch on
The PEM stack runs on AC 380 V and gas pressure builds to a steady 0.2 MPa.
Light the torch
Open the needle valve, ignite — and weld, braze, polish or cut.
Tell us what you weld or cut
Send us your material, thickness and daily working hours — we will recommend the right model from the 1500 to 15000 L/H range and send the data sheet and quotation.